Copper-nickel CuNi10(B10)
| Standaardisering: | Getalsimbool: | |
| GB/T9460-2008 | SCu7061 | |
| BS EN ISO24373:2009 | CuNi10 | |
| VANAF 1733 | SG-CuNi10Fe | |
| BS Chemical Composition: | % | |
| Cu incl.ag | bal. | |
| Mn | 0.50-1.50 | |
| Fe | 0.50-2.00 | |
| En | max 0.20 | |
| Ni incl.Co | 9.00-11.00 | |
| P | max 0.02 | |
| Pb | max 0.02 | |
| Ti | 0.10-0.50 | |
| C | max 0.05 | |
| S | max 0.02 | |
| Totaal ander | max 0.40 | |
| Fisiese eienskappe van materiale: | ||
| Digtheid | Kg/m^3 | 8.9 |
| Smeltbereik | ℃ | 1100-1145 |
| Termiese geleidingsvermoë | W/m.K | 30 |
| Elektriese geleidingsvermoë | S.m/mm^2 | 2.8-3.2 |
| Koëffisiënt van termiese uitsetting | 10^-6/K(20-300℃) | 17.0 |
| Standaardwaardes van die sweismetaal: | ||
| Verlenging | % | 34 |
| Treksterkte | N/mm^2 | 300 |
| Gekerfde staaf impak werk | J | 190 |
| Brinell hardheid | HB 2.5/62.5 | 80 |
| Aansoeke: | ||
| Used for welding of wrought to themselves or to each other.These filler metals also are used for welding the clad side of copper nickel clad steel.Preheating gernerally is not necessary.Welding is done in all positions.The arc should be kept as short as possible to assure adequate shielding gas coverage and thus minimize porosity.It may be used for surfacing applications where high resistance to corrosion,erosion is required. | ||
| Make-up: | ||
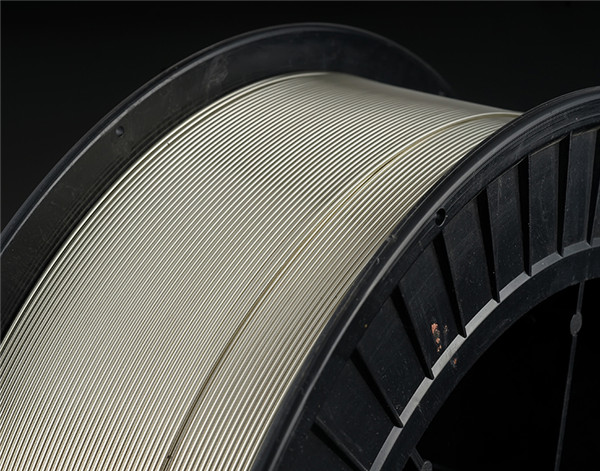
| Deursnee:1.00 – 1.20 – 1.60 -2.40 | ||
| Spole:D300 | ||
| Stawe:1.60 – 9.6 mm x 914/1000 mm | ||
| Verdere grimering op versoek. | ||
BS EN ISO24373:2009 CuNi10
Los jou boodskap